Engineering Superior Thermal, Acoustic, and Cryogenic Insulation Systems with Unrivaled Information Gain, E-E-A-T Compliance, and Direct Factory Supply for Annaba's Industrial & Commercial Hubs.
Industrial Whitepaper: Rubber Foam Insulation in Annaba
A Comprehensive Market Analysis, Technical Specification, and Direct-from-China Factory Procurement Blueprint for Annaba's Rapidly Expanding Industrial Ecosystem.
Strategic Context of Annaba’s Industrial Landscape
Annaba, strategically positioned as a premier economic, metallurgical, and maritime port hub in northeastern Algeria, demands resilient infrastructure solutions. From the heavy steel manufacturing complexes and complex chemical processing units to sprawling commercial real estate, HVAC systems, and cold chain logistics, the requirement for high-performance thermal insulation has never been more critical. Extreme seasonal temperature fluctuations coupled with high maritime humidity necessitate advanced closed-cell elastomeric rubber foam insulation accessories that resist moisture ingress, inhibit condensation, and withstand rigorous industrial operational stress.
As an authoritative manufacturer and factory powerhouse with over 45 years of accumulated industry mastery through our parent group, we bridge the gap between advanced Chinese manufacturing scalability and Annaba’s demanding localized engineering codes. Our specialized rubber foam products and auxiliary accessories are engineered to meet strict international standards, ensuring maximal energy efficiency, extended service lifecycles, and superior acoustic dampening across all construction and industrial environments.
Core Featured Solutions for Annaba Infrastructure
Essential Rubber Foam Insulation and Accessories Engineered for Maximum Thermal Resistance
Quantifiable Proof of Global Reliability, Production Capacity, and Supply Chain Dominance
5
Automatic Assembly Lines
600K+
m³ Annual Production
230+
Production Workers
88+
Countries Served
45+
Years of Development
Heritage & Direct Factory Authority
Established through the Jinwei Group (originally founded in 1979), Kingflex stands as a pioneer in thermal insulation materials. As the premier manufacturer north of the Yangtze River, we combine decades of metallurgical and chemical engineering experience to deliver robust insulation solutions customized for high-temperature and cryogenic projects worldwide.
Our dedicated R&D department features 8 senior professional engineers constantly optimizing formula resilience, thermal conductivity ratings, and flame-retardant performance to satisfy rigorous European and African import criteria.
Localized Support & Global Compliance
For industrial partners operating in Annaba, seamless logistics and unwavering product reliability are vital. Our products are fully certified under international benchmarks including BS 476, CE, REACH, ROHS, UL94, and ASTM standards.
We provide full documentation, batch traceability, and custom OEM/ODM packaging options to ensure that contractors, project specifiers, and procurement directors in Annaba receive exact-match specifications for their mechanical and civil engineering projects.
In-Depth Performance Metrics of Our Flagship Elastomeric Rubber Foam Materials
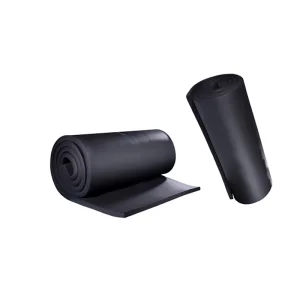
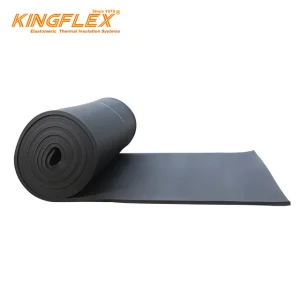
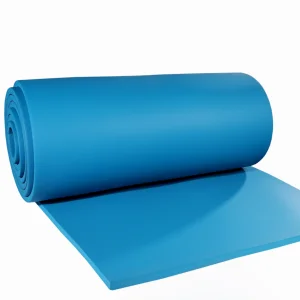
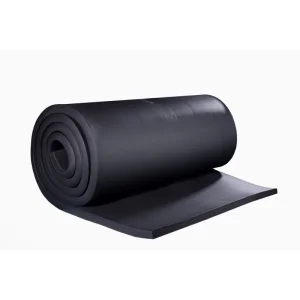
Black Rubber Foam Insulation Sheet Roll
Standard Dimension & Parameters:
Material: NBR/PVC | Thickness: 6mm - 50mm | Density: 40 - 55 kg/m³ | Service Temperature: -40℃ to 105℃
Core Advantages:
1. Uniform foaming structure with a closed-cell rate exceeding 98%, blocking moisture penetration.
2. Exceptional compression resilience over 80%, ensuring long-term structural integrity.
3. Flame retardant and self-extinguishing upon fire source removal.
4. Low thermal conductivity coupled with high moisture resistance factor.
Annaba Application Scenarios:
Ideal for central air conditioning ductwork, industrial plant storage tanks, chemical processing pipeline insulation, and commercial building soundproofing.
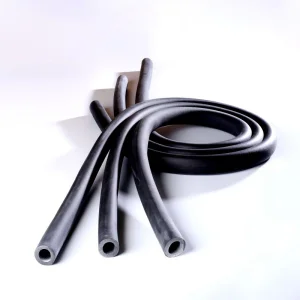
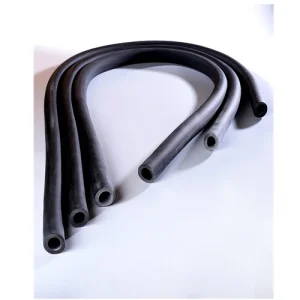
Standard Dimension & Parameters:
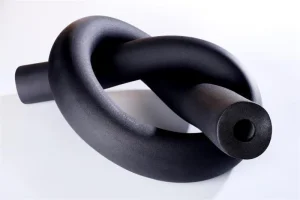
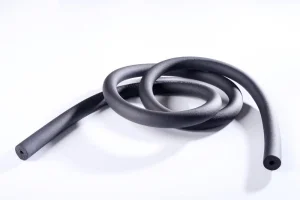
Material: NBR/PVC | Thickness: 9mm - 40mm | Inner Diameter (ID): 6mm - 114mm | Density: 40 - 55 kg/m³ | Service Temperature: -40℃ to 105℃
Core Advantages:
1. Automated precision coating ensures consistent thickness and seamless finish.
2. Superior anti-condensation performance, drastically reducing pipe corrosion and cracking risks.
3. High flexibility for rapid, labor-saving installation on complex piping geometries.
Annaba Application Scenarios:
Widely utilized in chilled/hot water piping for marine vessels, industrial cooling systems, hotel HVAC networks, and municipal water supply lines across Annaba.
Expert Answers to Common Procurement and Technical Inquiries for Annaba Clients
Q1: What is elastomeric rubber foam insulation used for?
A1: It is mainly used for HVAC ducts, air conditioning pipes, building thermal insulation, industrial pipeline cold insulation, and acoustic sound dampening in commercial and heavy industrial facilities.
Q2: Is Kingflex rubber foam insulation fire resistant?
A2: Yes, our rubber foam insulation products are inherently fire retardant and self-extinguishing, meeting stringent safety standards for building and industrial projects.
Q3: What is the difference between rubber foam and rock wool insulation?
A3: Rubber foam is flexible, closed-cell, and moisture-proof, ideal for HVAC and cold insulation; rock wool is high-temperature resistant and fireproof, designed for industrial high-heat pipelines.
Q4: Do you provide customized insulation products?
A4: Yes, we fully support OEM and custom manufacturing services to precisely meet unique project specifications in Annaba and international markets.
Q5: What certifications do your products hold?
A5: Our products have passed BS 476, CE, REACH, ROHS, UL94, and ASTM international certifications, guaranteeing compliance with global quality and safety benchmarks.
Q6: Does Kingflex offer product traceability?
A6: Yes, all Kingflex manufactured insulation materials include rigorous batch traceability from raw material selection to final dispatch.
Q7: What thickness range of rubber foam sheet roll is available?
A7: We produce high-performance elastomeric rubber foam sheet rolls in thicknesses ranging from 6mm up to 50mm to suit diverse insulation values.
Q8: What is the typical service life of rubber plastic pipes and boards?
A8: Under standard operational conditions and proper installation, our rubber foam insulation materials provide a reliable service life of approximately 10 to 15 years.
 Kingflex